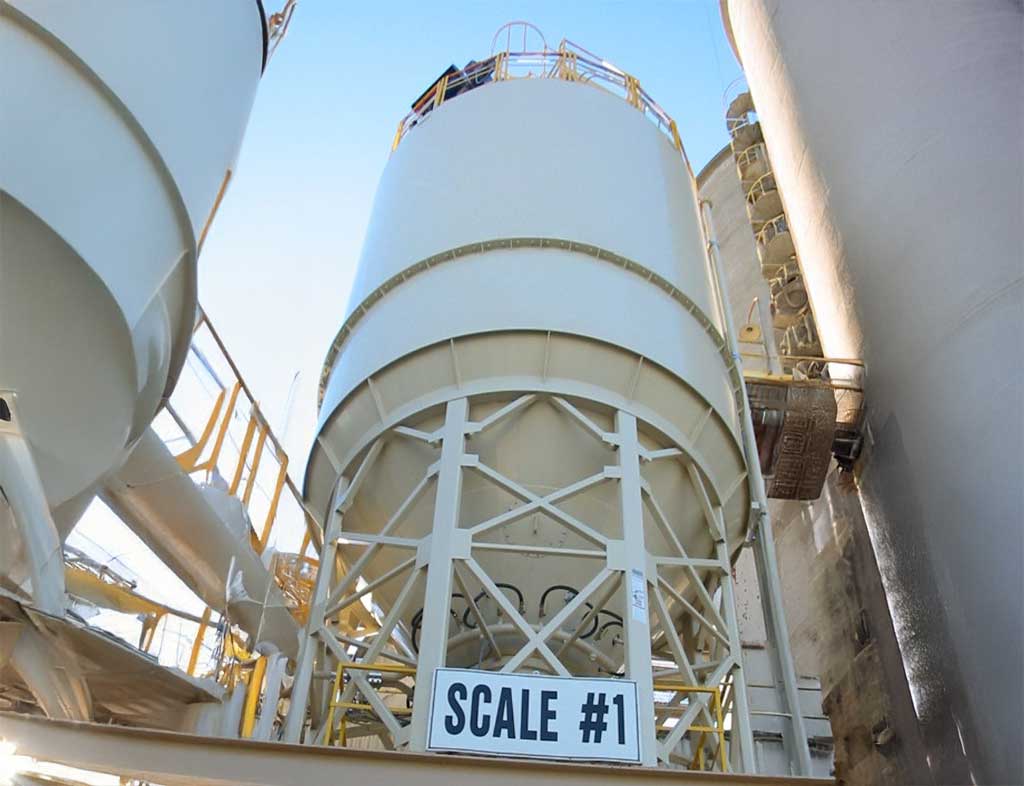
Mining isn’t for the faint of heart. Whether you’re pulling potash from the prairies or blasting rock in the Rockies, you need a storage system that can hold up to the dust, weight and weather that come with the job. Meridian Manufacturing builds silos for some of the toughest industrial applications on the planet. From bolt‑together giants that hold enough material to fill a warehouse to specialty vessels designed for ammonium nitrate and emulsion explosives, Meridian’s lineup offers mining operations a safe and reliable place to store what keeps their operation moving.
Before diving into specific models, it helps to understand what sets Meridian apart. Their industrial bins are built from heavy‑gauge steel and finished with a thick powder‑coated paint. Powder coating outperforms standard paints by offering superior corrosion resistance and weather protection. Meridian’s quality welds and thick powder coating give contractors confidence that the tanks will stand up to tight deadlines and harsh environments. Meridian silos also feature a seamless interior—there are no bolts, ribs or corrugations inside—so product doesn’t hang up or cross‑contaminate during discharge. This smoothwall design makes sense for mining because it speeds clean‑out and reduces the risk of bridging.
Meridian works closely with each customer to tailor the silo or tank to their site and their material’s storage requirements. Whether you need remote installation, special liner coatings or integrated catwalks, the company’s engineers can design a solution to meet regulatory requirements and operational needs. Let’s look at three silo families that stand out for bulk storage in mining.
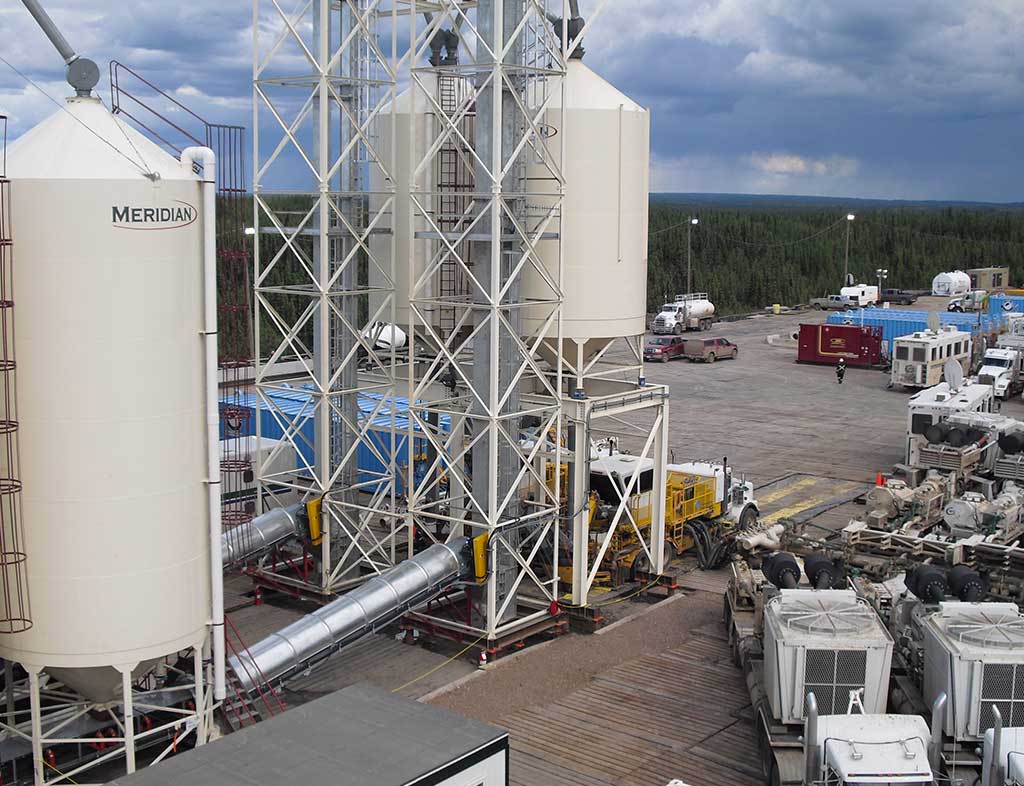
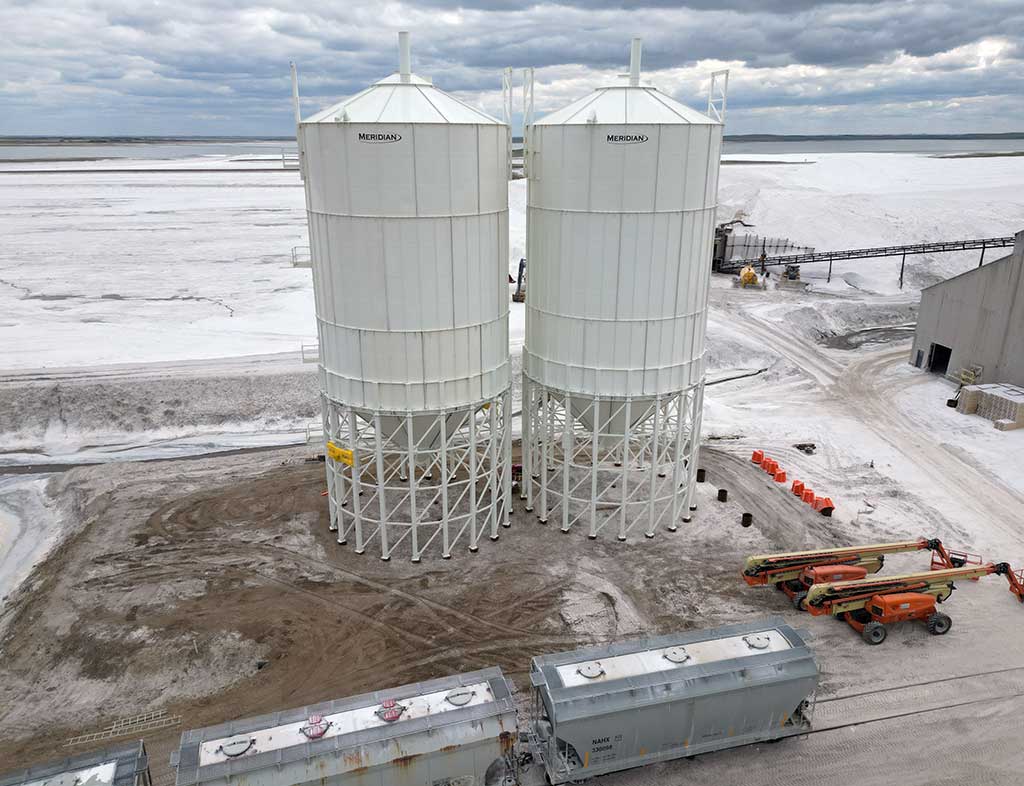
Large mines move huge volumes of ore, concentrates, reagents and tailings. Transporting and erecting a single‑piece storage vessel that can hold tens of thousands of cubic feet is almost impossible, especially in remote areas. Meridian’s bolt‑together silos solve that problem. Instead of shipping a welded bin in one piece, bolt‑together models arrive on site as flat‑packed panels that are assembled in place. These silos are engineered for situations where transportation, site access limitations, or capacity needs make single‑piece construction impractical. Panels ship flat so they’re easy to haul into hard‑to‑access locations, and the silos are assembled with full perimeter reinforcement for strength.
Key benefits include:
Because bolt‑together silos ship in pieces, they can be hauled down a mine road with standard equipment. Once on site, the panels are lifted into place and secured with structural bolts. Modular installation also means you can expand capacity later by adding rings or increasing height. For mines with changing production rates, this scalability is a game changer—build what you need now and add to it as site expansion requires. Combine the huge capacity with accessories such as pneumatic fill systems, spiral staircases, drive‑through load‑outs and OSHA‑approved ladders, and you have a turnkey storage hub designed for industrial safety.
If your operation relies on ammonium nitrate (AN), safe storage is more than convenience—it’s a legal requirement. AN is hygroscopic and can be unstable if contaminated, so the tank must keep the product dry, clean and secure. Meridian’s SmoothWall Ammonium Nitrate Silos are purpose‑built for the job. These silos are manufactured with high‑quality steel and finished with a superior powder coat to provide rugged, reliable, and weatherproof storage. The seamless interior means there are no bolt heads or seams for AN prills to get hung up on; unloading is smooth and contamination‑free.
Features of Meridian’s AN silos include:
Typical units range from around 2,700 cubic feet for a 13‑ft diameter silo up to more than 8,700 cubic feet for an 18‑ft diameter model. Capacities can exceed 230 metric tonnes, giving mine sites plenty of supply for shot‑firing without constant deliveries. The powder‑coated exterior stands up to weather, while the interior coating resists the corrosive nature of AN. For explosive products like ammonium nitrate/fuel oil (ANFO), pairing an AN silo with a Meridian Emulsion Silo makes on‑site blending safer and more efficient.
Bulk emulsion explosives are widely used in surface and underground mines because they are safer to handle than dry ANFO. However, the emulsion must be stored in vessels that protect it from moisture, contamination and pressure variations. Meridian supplies SmoothWall Emulsion Silos that can be relied on for the long run and are engineered to your specific application. Meridian builds these silos with options like standard stand‑alone tanks or overhead load‑outs with a drive‑through structure. That flexibility allows you to set up a portable explosives plant right at the mine.
Notable features include:
Capacities start around 2,080 cubic feet and scale up for larger operational needs. Because the tanks are fully welded and pressure tested, they maintain integrity even when loaded with dense emulsions. Powder coating both inside and out minimizes corrosion and contamination, which helps maintain the emulsion’s chemical stability.
While bolt‑together, ammonium nitrate and emulsion silos cover the main explosive and reagent needs, Meridian offers other tank types that help mining operations run smoothly.
Combining these storage solutions with conveyors, augers and bulk bag unloaders creates an integrated material handling system tailored to a mine’s processes.
Choosing the right silo isn’t just about picking a size off a chart; it’s about understanding your material and how it flows through your operation. Meridian’s team will ask questions about bulk density, flow characteristics, required discharge rates and site conditions. Bolt‑together silos shine when capacity is king and logistics are challenging. SmoothWall ammonium nitrate silos meet strict explosive handling regulations, while emulsion silos support on‑site blending and storage. Sand and aggregate bins round out material handling for road building, backfill and processing.
When planning a storage installation, consider how the silo will feed downstream equipment. Meridian offers accessories like butterfly or slide gates, pneumatic fill systems, skids for mobility, spiral staircases and integrated catwalks. For explosive products, proper grounding, venting and monitoring systems are essential. Local regulations may dictate setbacks, foundation design and safety features. Working with Meridian and their experienced partners ensures the installation meets all codes and integrates smoothly with your conveyor and processing systems.
Mining operations demand rugged, high‑capacity storage that can be deployed quickly and safely. Meridian Manufacturing’s silos rise to the challenge. Bolt‑together units deliver modular scalability and enormous volume in areas where transporting a single‑piece tank would be impossible. SmoothWall ammonium nitrate and emulsion silos provide purpose‑built solutions for explosives, combining seamless interiors with heavy‑duty construction and durable powder coating. Additional sand, aggregate and cement silos round out a complete material handling system.Meridian’s silos are strong and meant to last. They’re built by folks who understand that remote sites demand equipment that just works, no matter the weather or the payload. If you’re looking to boost efficiency, improve safety and keep your bulk materials where they belong, it’s worth having a chat with Meridian about the right silo for your mine. As the saying goes, big jobs need big solutions, and these silos are ready to do the heavy lifting.
If your project involves bulk storage challenges, our team is ready to help. Contact us to discuss your specific requirements and explore how our bolt‑together, ammonium nitrate and emulsion silos, or custom engineered solution can be help with your operational needs. Were here to ensure your storage solution meets the demands of your mining operation.